+86 180 0293 5268


Aerospace Machining suppliers face a demanding market: buyers need precise parts, dependable delivery, and clear evidence of process control. Boeing’s 2024 Commercial Market Outlook forecasts 43,975 new aircraft deliveries between 2024 and 2043. That projection signals long-term production needs, but it is not a direct forecast of machining demand. Aircraft programs, replacement cycles, and supplier qualifications all shape the real opportunity.
The details matter. A titanium bracket may look simple on a drawing, yet thin walls, tight tolerances, and heat during cutting can complicate production. Buyers should assess material experience, inspection capability, traceability, delivery performance, and communication—not just hourly rates. Quality expert W. Edwards Deming offered a useful principle: “Quality comes not from inspection, but from improvement of the production process.” For aerospace buyers, that means asking how a supplier controls work before a part reaches final inspection.
There is no perfect supplier checklist. A polished capability sheet can hide weak scheduling, and a small shop may deliver excellent work but lack backup capacity. That deserves a closer look. This guide compares suppliers through practical criteria, including machining capabilities, quality systems, materials, and support for global buyers. Use it as a starting point, then verify claims directly with each supplier. A brochure is not a production record.
Aerospace machining suppliers turn engineering drawings into flight-critical components through CNC milling, turning, drilling, and precision finishing. They may produce brackets, housings, structural fittings, or engine-related parts from aluminum, titanium, and specialty alloys. The work involves more than cutting metal. Teams review drawing revisions, confirm material specifications, control tool wear, and inspect features such as bore diameter, flatness, and hole position. Small deviations can affect assembly, so inspection records matter.
AS9100 is a widely used aerospace quality-management standard, built on ISO 9001 with additional industry requirements. It supports risk management, configuration control, corrective action, and traceability. Suppliers may also use AS9102 first article inspection to document that a new or revised part meets its drawing. Calibration records, material certificates, and inspection reports help buyers follow a component’s history. Nadcap accreditation may apply when a supplier performs covered special processes, but it is not a general machining certificate. Scope matters.
A certificate is useful, but not magic. Buyers should check that the supplier’s approvals cover the actual site and processes involved. Ask how it handles drawing changes, nonconforming parts, and measurement uncertainty. A polished audit file can still leave practical questions unanswered. One clear sample inspection report often tells you more.
2026 Best Aerospace Machining Suppliers for Global Buyers?
How to Assess Machining Capabilities for Aerospace Components
Assess more than a supplier’s machine list. Ask for evidence that its processes can repeatedly hold your drawing tolerances. Review equipment capability, material traceability, inspection plans, and nonconformance records. For a five-axis part, check how the supplier controls setups and verifies features that are difficult to reach. A polished audit is useful, but it cannot prove every complex component will run smoothly.
Quality systems matter. Check current AS9100 certification, calibration records, and first-article inspection practices. The Aerospace Industries Association’s 2024 Facts & Figures reports about $955 billion in U.S. aerospace and defense sales for 2023, underscoring the scale of this supply chain. That figure is not a measure of machining demand, but it highlights why buyers should verify capacity, subcontractor controls, and delivery history. Request sample inspection reports and confirm that measured results match the component’s critical features.
Tips: Send a representative drawing and material specification during evaluation. Ask how the supplier handles tool wear, dimensional drift, and late engineering changes. Then compare its answers with a small pilot run. Paperwork helps. Parts tell more.
Aerospace programs rarely need the same machining partner. Prototype teams often benefit from flexible job shops that can adjust a fixture or revise a toolpath quickly. They may produce only a few brackets or housings, so clear engineering communication matters more than sheer machine count. Ask how the supplier handles drawing changes, first-article inspection, and material traceability. Small details matter.
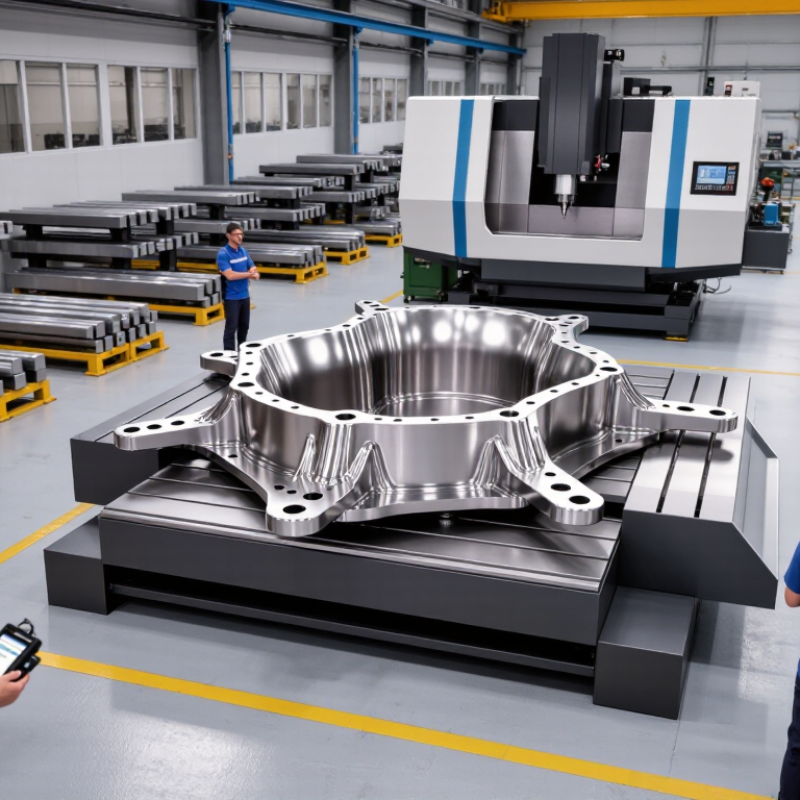
Recurring commercial programs usually need suppliers with stable capacity, repeatable inspection methods, and documented process controls. A delivered part should match its approved drawing, not just look right on a bench. For large structures, buyers may need shops equipped for long-bed milling and careful handling of oversized aluminum parts. For complex, close-tolerance components, look for suitable metrology equipment and inspection records that link results to each production lot. Still, a polished audit file cannot guarantee a smooth launch. Confirm lead times against actual capacity, and discuss what happens when a tool wears or a batch fails inspection. The best fit depends on program volume, part geometry, risk, and the buyer’s own review process. It is easy to overvalue a machine list. People, planning, and honest reporting count too.
Choosing an aerospace machining supplier in 2026 takes more than comparing hourly rates. Start with the part’s actual requirements: alloy, tolerance, surface finish, annual volume, and inspection level. Ask how the shop controls drawing revisions and connects each lot to material certificates, machine records, and inspection results. Traceability matters when a drawing changes mid-production. Details matter.
Compare evidence, not polished claims. Request a sample inspection report, calibration status, and a first-article process relevant to your component. For a thin-wall bracket, ask how distortion is checked after machining, not only whether a machine can hold a stated tolerance. Review how nonconformances are handled and corrective actions documented. A site visit may reveal chip management, tool-wear checks, and whether operators use consistent setup sheets. No scorecard is perfect.
Capacity and communication deserve equal attention. Confirm realistic timing for raw material, programming, first-article inspection, and repeat orders; one quoted lead time can hide several bottlenecks. Ask who approves changes and how quickly you will hear about a broken tool or delayed material lot. Compare total risk, not only unit price. A small pilot run can expose gaps before critical production begins. It may add time, but skipping it can leave assumptions untested.
How to compare aerospace machining suppliers in 2026: assess quality systems, technical capability, delivery performance, compliance, and communication against your part requirements.
Illustrative buyer scorecard weighting—not supplier performance data or an industry-wide survey. No universal public dataset sets standard weights for these criteria; adjust the percentages to your program’s risk, specifications, and sourcing priorities.
Qualifying an aerospace machining supplier takes more than reviewing a capability list. Ask for recent inspection reports, material certificates, and examples of how nonconforming parts were handled. A sample component can reveal practical details: edge finish, bore consistency, and whether measurement results match the drawing. Check that inspection equipment is calibrated and that operators understand the required tolerances.
Look beyond the first article. Review how the supplier controls revisions, tracks material lots, and protects parts during storage and shipping. Discuss realistic capacity using machine availability, staffing, and planned maintenance—not a sales estimate alone. Request clear lead-time updates and an agreed process for reporting delays. Keep records of decisions and approved changes. Details matter.
A polished audit can still miss everyday problems. Small communication gaps, such as an unclear drawing revision, can create costly rework. Set regular reviews around delivery performance, quality trends, and corrective actions. Share forecasts early, but avoid assuming every urgent request can be absorbed. Build a backup plan for critical operations. No supplier is flawless; transparent evidence and steady follow-up make weaknesses easier to address before they disrupt production.
| Qualification Dimension | Evidence to Request | How Buyers Can Verify | Suggested Qualification Decision Rule | Ongoing Supplier Management |
|---|---|---|---|---|
| Quality management system | Current quality-system certificate and defined scope covering the relevant manufacturing site and processes. Aerospace buyers commonly specify AS9100-series requirements; ISO 9001 alone may not meet a contract’s aerospace quality requirements. | Check certificate validity, site address, scope, and certification status with the issuing certification body. Confirm that the audited site is the site that will perform the work. | Require the quality-system level stated in the purchase contract or customer flow-down. Do not treat a certificate as proof that a specific part or process is capable. | Track certificate expiry, major audit findings, corrective-action closure, and changes to site or scope. |
| Technical capability and process control | Process flow, equipment list, capability statements, work instructions, tooling controls, maintenance records, and examples of comparable part families. | Review the process route and conduct a technical assessment of the actual production site. Confirm machine, fixture, tool, and program controls against drawing and specification requirements. | Approve only the processes, part families, and manufacturing locations demonstrated during assessment and agreed in the contract. | Require prior approval for material changes to equipment, process route, production location, or subcontracting. |
| Measurement and inspection | Inspection plans, calibrated-equipment register, measurement-system records, CMM or other inspection capability, and sample inspection reports. | Check calibration traceability and status. Review whether inspection methods and measurement uncertainty are appropriate for the specified tolerances and features. | Require documented evidence that all drawing and specification characteristics can be inspected using suitable, controlled methods. | Monitor calibration status, inspection escapes, nonconformances, and completion of corrective actions. |
| First article inspection | A first article inspection report prepared to the contractually required format. AS9102 is a commonly specified aerospace first article inspection standard. | Check that the report accounts for drawing characteristics, material and process records, and any customer-required documentation. Confirm revision and configuration alignment. | Require customer approval or acceptance where the contract calls for it before authorizing production release. | Apply the contract’s rules for repeat first article inspection after defined design, process, tooling, or production-location changes. |
| Material traceability and configuration control | Material certificates, heat or lot identification, purchase records, receiving inspection records, and procedures for preserving identity through production. | Trace a sample finished part back to its material lot and applicable process records. Verify drawing revision and change-notification controls. | Require complete, legible traceability and configuration records for each lot or part as defined by the contract. | Review traceability samples, record-retention compliance, and the handling of engineering changes and obsolete revisions. |
| Special processes and subcontractors | Approved-source details, process specifications, certificates, and subcontractor flow-down records for processes such as heat treatment, surface treatment, or non-destructive testing when applicable. | Verify that the processing source and process approval meet the customer’s specifications and approved-source requirements. Confirm that records link to the relevant part or lot. | Do not release work to an unapproved source where customer approval or a specified accreditation is required. | Maintain an approved-source list and require notification and approval before changes to special-process sources. |
| Nonconformance and corrective action | Documented nonconformance procedure, containment process, root-cause method, corrective-action records, and customer notification controls. | Review representative closed cases for effective containment, evidence-based cause analysis, corrective action, and effectiveness checks. | Require prompt containment and timely, documented disposition of nonconforming product under the applicable contract and customer requirements. | Trend defects, escapes, repeat findings, and overdue corrective actions; escalate recurring or safety-critical issues. |
| Delivery and capacity | Capacity plan, current workload, lead-time assumptions, staffing coverage, critical-equipment dependencies, and business-continuity arrangements. | Compare proposed capacity with forecast demand and production constraints. Review delivery history using an agreed definition of on-time delivery. | Agree realistic capacity and lead times in writing; assess resilience for constrained machines, materials, and sub-tier processes. | Review delivery performance, backlog, forecast changes, and recovery plans at an agreed cadence. |
| Export controls and information security | Documented process for classifying, accessing, storing, and transferring controlled technical data, where applicable to the transaction. | Determine applicable export-control and data-security obligations with qualified legal and compliance personnel. Verify access controls and approved data-transfer methods. | Release controlled data only after applicable legal, contractual, and customer requirements are confirmed and controls are in place. | Review access authorization, incident reporting, personnel training, and subcontractor data handling as required by the contract. |
| Commercial and global supply risk | Quotation assumptions, payment and currency terms, shipping responsibilities, packaging requirements, insurance details, and continuity or recovery plans. | Clarify delivery terms, customs responsibilities, import documentation, packaging, and agreed escalation contacts before purchase-order release. | Document responsibilities, risks, and remedies in the contract; avoid relying on verbal commitments for critical requirements. | Review cost changes, shipping disruptions, financial or operational risk signals, and continuity-plan updates. |